Touch Probe Setup and Calibration
A touch probe is a fast and convenient way to indicate a workpiece: you can pick up an edge in one motion, in any direction, without the spinning and the tip-radius math of an edge finder. It is only as accurate as its setup, though. The values TouchDRO stores for the probe (the effective tip diameter and the offsets) describe the probe as it sits in your spindle, not the instrument in the box, so if the probe is mounted loosely, sits off the spindle axis, or is set up with the diameter printed on the box instead of a measured one, every edge it finds will be off by the same amount.
Set up properly, the same probe will indicate a workpiece, find the center of a bore, or pick up the centerline of a part to within a count or two of your scales. The setup only has to be done once, as long as the probe goes back into the spindle the same way each time.
This guide covers the three steps: mounting the probe so the measurements stay valid, centering its trigger point on the spindle axis, and calibrating the effective tip diameter with the calibration wizard and a ring gauge. Do them in that order, since each one depends on the one before it.
Before You Start
The probe needs to be wired to the adapter's probe input, as described in the "TDA-4xx DRO Adapter Manual", and it needs a probe profile with its trigger source set to the port it is wired to. Enter the nominal tip diameter from the box when you create the profile; calibration will replace it with a measured value at the end of this guide.
Mounting the Probe
Unlike a spinning edge finder, a touch probe has no way to ignore the runout (TIR) of the spindle and the collet. In order to get repeatable accuracy, the probe needs to be mounted repeatably. On a manual milling machine this usually means using the same collet, clocking the spindle to the same position, and inserting the probe facing the same way.
Hold the probe in a collet or a dedicated holder rather than a drill chuck, since a chuck will not hold the same orientation twice, and keep the probe in the collet it was measured in. If you take the probe out together with its holder and store the pair as one piece, the setup work below survives tool changes, and the only thing left to get right each time is the orientation in the spindle.
Centering the Probe in the Spindle
A probe doesn't strictly need to be coaxial with the spindle, as long as its position in the spindle is repeatable: TouchDRO can store the offset in the probe's profile. Spending a bit of time carefully centering the probe still pays off, because it reduces the error you get from imperfect clocking. The closer the trigger point sits to the spindle axis, the less it matters if the probe goes back in turned slightly from where it was measured, and with a well-centered probe you leave the profile offsets at zero.
Adjust the probe until it is as close to concentric as you can get it: most probes have adjustment screws on the head for exactly this, and the probe's own manual will describe how to use them.
Note that what has to be centered is the point at which the probe triggers, and an indicator can't find that point. An indicator reads the surface of the stylus ball under a fraction of an ounce of pressure, while the trigger point is where the stylus has deflected far enough to open the switch, which takes real force and doesn't necessarily happen where the ball's surface suggests. As a result, a probe that indicates perfectly can still trigger off-center.
The only instrument that applies the right force is the probe itself, so the check is done with the probe:
- With the probe clocked the way you normally use it, indicate an edge on a workpiece and set the absolute origin there.
- Rotate the probe 180 degrees in the spindle.
- Indicate the same edge again.
- Read the difference. If it is zero, the trigger point is on the spindle axis.
Any difference is twice the error, because turning the probe around moves the trigger point across the axis rather than to it. Adjust the tip by the procedure in the probe's manual and run the check again. A few rounds of this is normal.
Calibrating the Tip Diameter
The nominal diameter marked on a 2D edge finder or a kinematic touch probe is a starting point. During probing, the forces acting on the stylus cause the trigger point to be offset from the true center of the stylus, and depending on the probe model the difference can range from negligible to tens of microns. TouchDRO measures the effective diameter based on the actual trigger point, which gives more accurate measurements.
Calibrate with the probe centered, as described above. The calibration process does not account for any misalignment of the probe, and if the probe is not centered, the calibration will yield inaccurate results.
What You Will Need
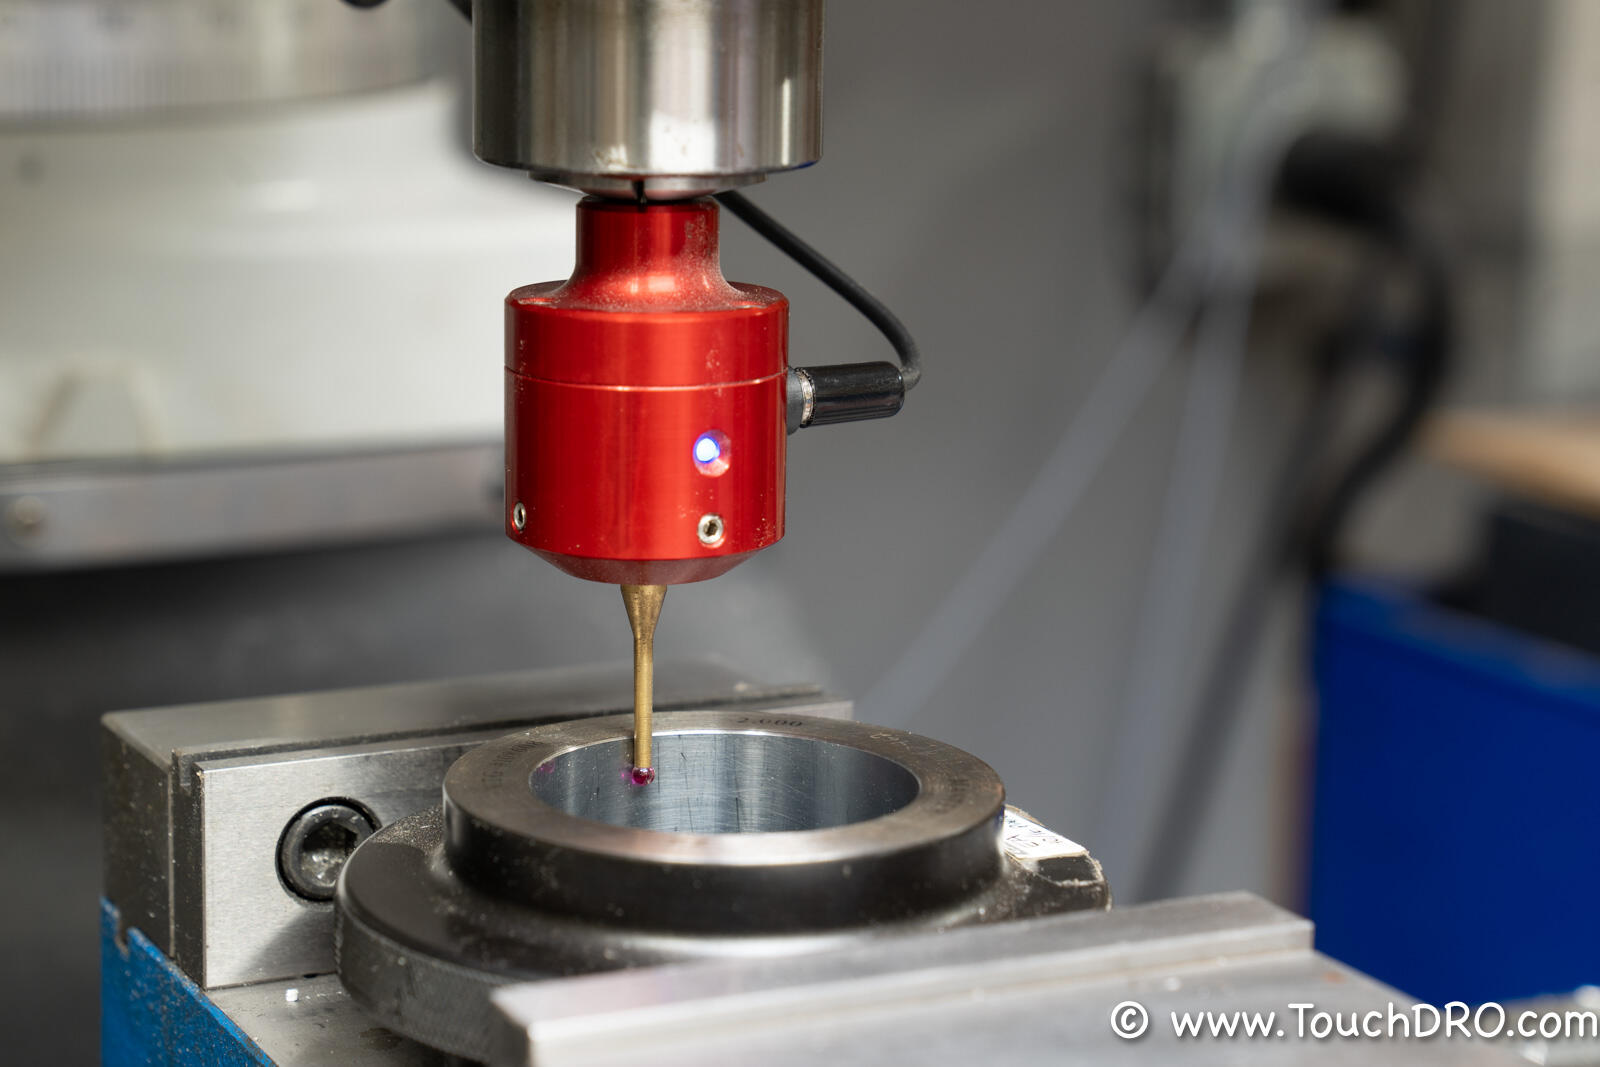
You will need a ring gauge, or any accurate bore of known diameter. The inner race of a precision ball bearing works and costs a lot less than a gauge. Keep it on the small side: something in the 1 to 2 inch range is the most convenient to work in.
Running the Wizard
Mount the gauge on the table and move the stylus roughly to the center of the bore. It doesn't have to be precise; within a few millimeters of the center is fine.
Keep the stylus at the same Z height throughout. Moving up or down between touches allows any tram error in the head to show up in the result, and the wizard can't tell that apart from a tip that isn't round.
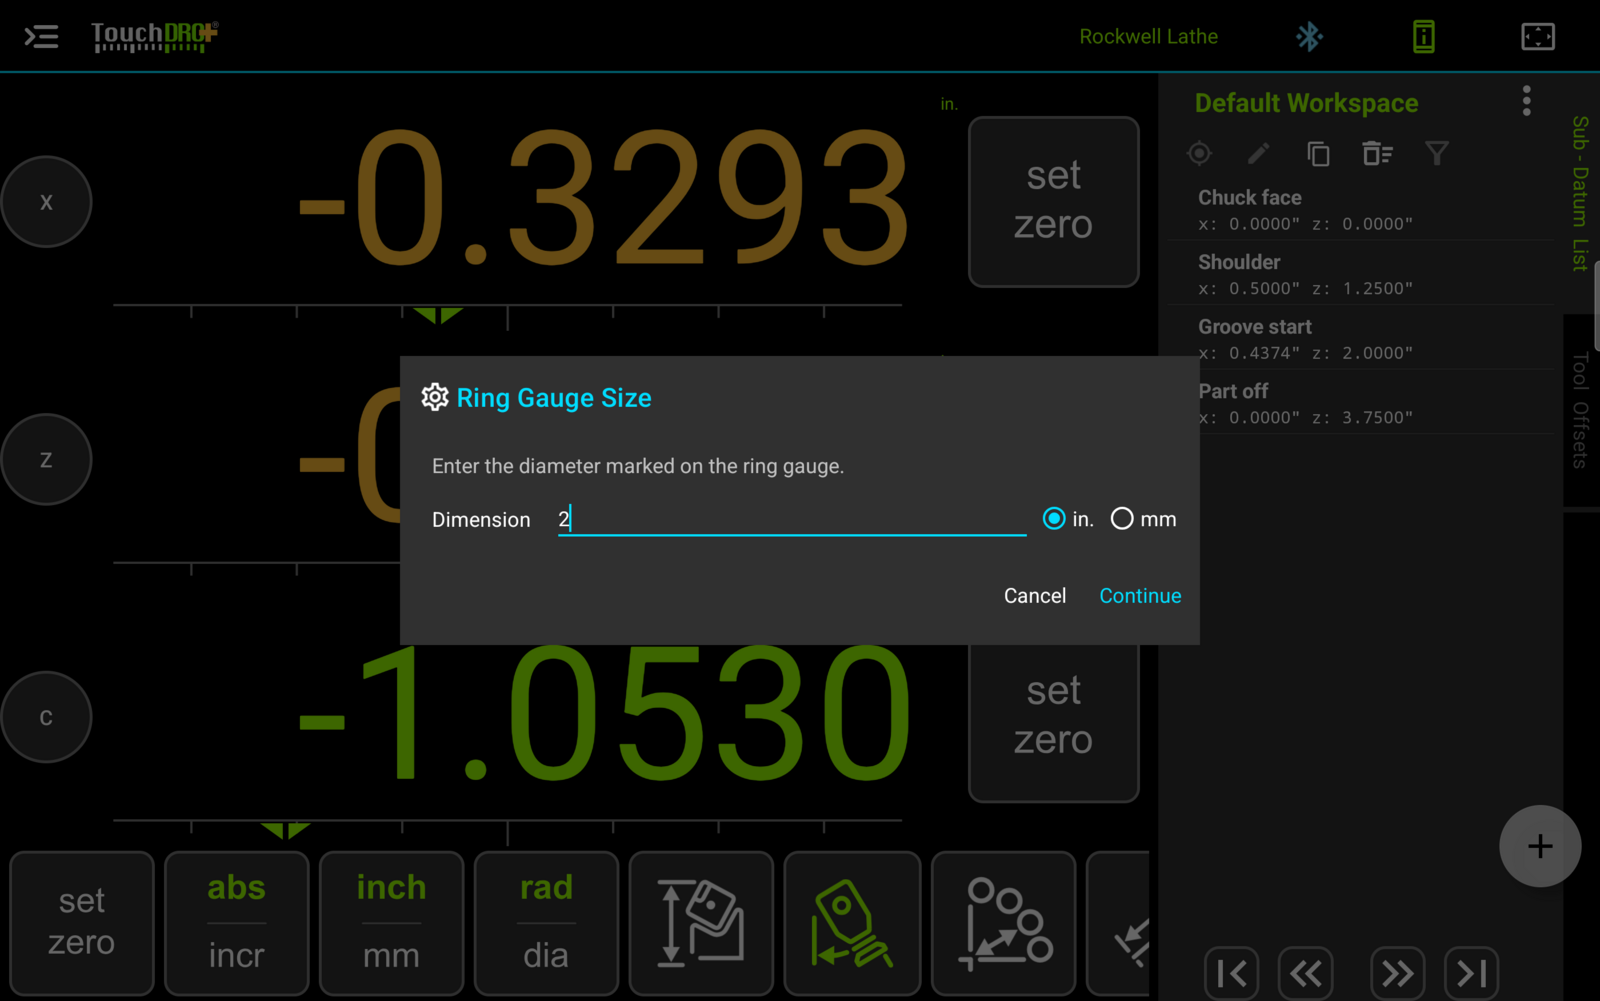
To start the wizard, open the probe's profile and press the calibration button beside the "Tip diameter" field, the one with the ruler icon. The wizard opens by asking for the gauge diameter.
The wizard will ask you to touch the ring gauge several times at each of four clock positions, taken in opposed pairs: 9 o'clock, then 3, then 12, then 6. This does several things at once. Besides calculating the effective diameter, it also measures how repeatable the touches are and how many it took to get there.
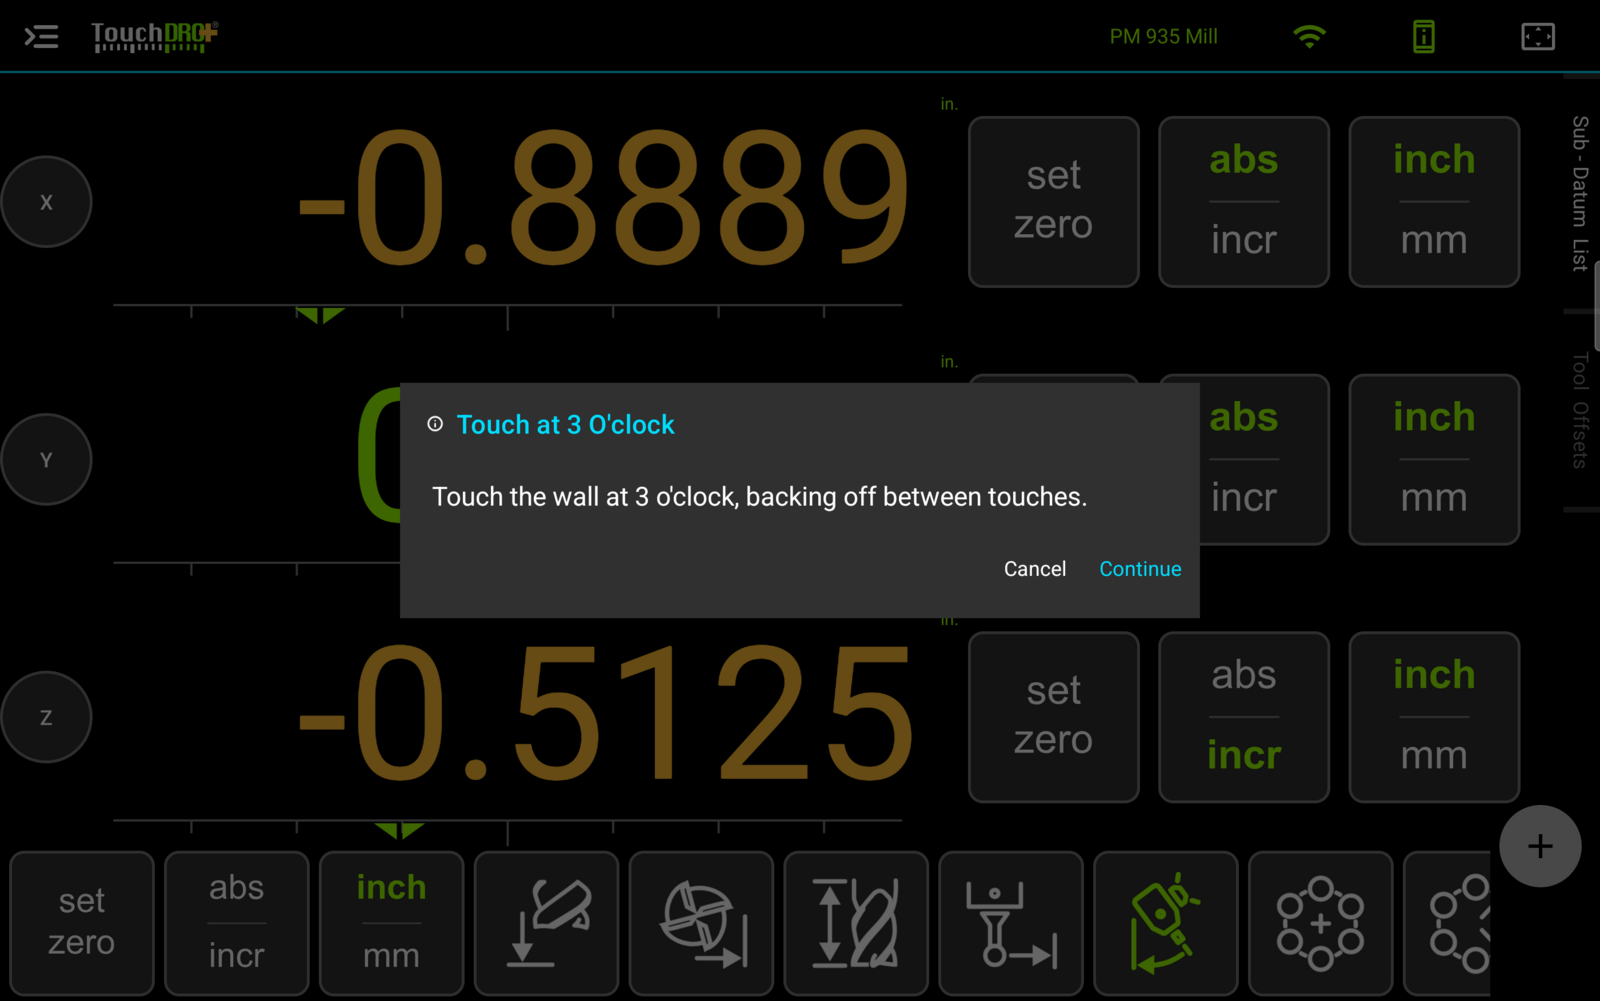
At each position, TouchDRO needs at least three touches to calculate the effective diameter, but doing more will give you a better result.
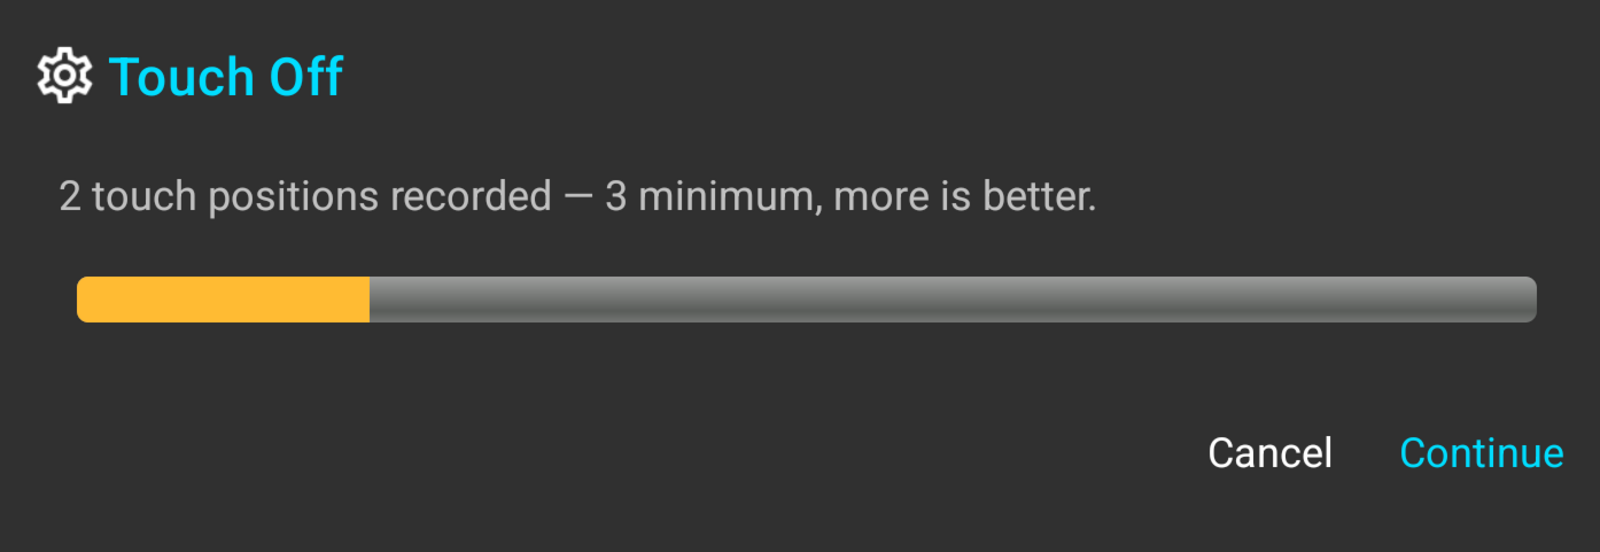
Once the third touch is in, the bar turns green and you can move on whenever you like. More touches give a better result, since the extra touches are what make the repeatability number meaningful, but stopping anywhere in the green is fine. The bar is full at ten touches, but that is not a limit; the wizard keeps recording any touches you take past it.
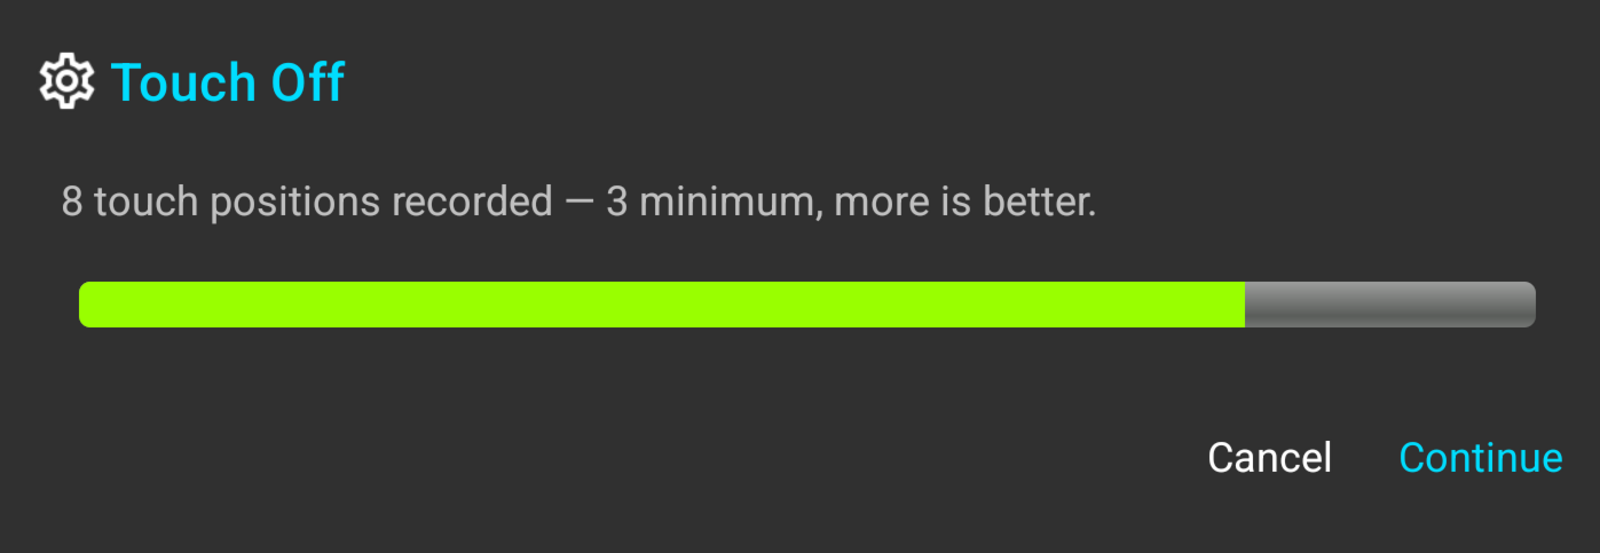
Between the pairs the wizard asks you to come back to the middle, showing a marker to crank against. After the 9 and 3 o'clock touches the bore's center in X is known exactly, and the stylus needs to be near it to reach the top and bottom of the bore cleanly without fouling the bore wall.
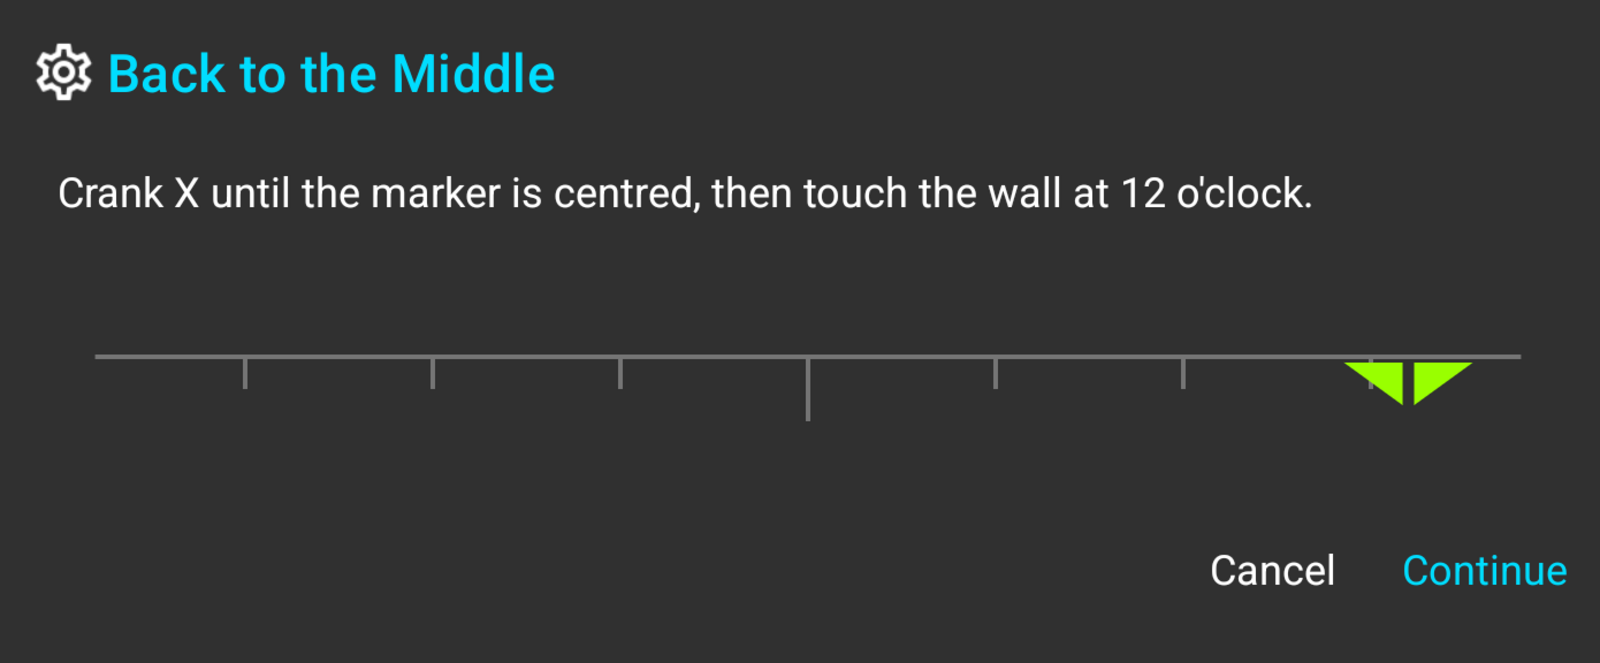
When all four positions are done, TouchDRO reports the effective tip diameter, how repeatable the touches were, how many it used, and the gauge size it worked from. "Apply" writes the diameter into the profile; "Discard" leaves the profile as it was.
The result can include one more paragraph, with the diameter measured across X and the diameter measured across Y shown separately. It is shown when the two differ by more than the run's own scatter, or by more than 10 µm, whichever is larger, on clean and warned results alike. See "Across X and Across Y" for what to make of it. The refusals described below never include it, since there is no result.
Calibration Failure Scenarios
TouchDRO checks the finished measurement before offering to save it, and there are four ways the check can come back other than clean. Three of them refuse the result, because the number can't be right. The fourth is a warning and only asks you to look again.
Cannot Fit a Circle
"Cannot Fit a Circle" means the four touches don't describe one. Points that fall in a line, or two touches taken at the same place, don't give the wizard enough to calculate a circle. Take them again, one at each clock position.
Tip Has No Size
"Tip Has No Size" means the circle the touches describe came out no smaller than the ring gauge you entered, which should be physically impossible with a properly functioning probe. The usual causes are a gauge diameter typed in wrong, and probing around the outside of something instead of inside a bore.
Unlikely Tip Size
"Unlikely Tip Size" means the calculation succeeded but the result is not a plausible stylus size. This one almost always comes back to the ring gauge value as well, most often a metric size typed into an imperial profile, or a decimal point in the wrong place.
Retry and Cancel
All three refusals offer "Retry" and "Cancel". Retry throws the four touches away and starts the capture over at the first clock position, keeping the gauge diameter you entered, so if one bad touch-off spoils a run, you only lose the touches. Cancel abandons the run and leaves the profile as it was.
The Diameter Mismatch Warning
The fourth outcome is a warning rather than a refusal. If the measured diameter is a plausible stylus size but lands more than a quarter of the entered diameter away from the diameter on the profile, TouchDRO shows the measured diameter next to the one in the profile and asks you to check the ring gauge. If the gauge value is right, the measurement stands, and you can save it.
The quarter threshold is intentionally loose, since pre-travel on a mechanical probe can run into hundreds of microns, and a measured diameter well away from the marked one is normal. The purpose of the check is to catch a wrong gauge number; it says nothing about how accurate the probe is. The check is also skipped on a profile with no tip diameter entered, since there is nothing to compare against.
Applying the Result
When you apply the result, TouchDRO writes the measured effective diameter into the profile's tip diameter field, and it also stores the run itself (the date, the gauge size, and the measured diameter) with the profile. Only the most recent applied run is stored, and calibrating again replaces it. The run is included in the export file for troubleshooting, so you can send it to TouchDRO support if you need help.
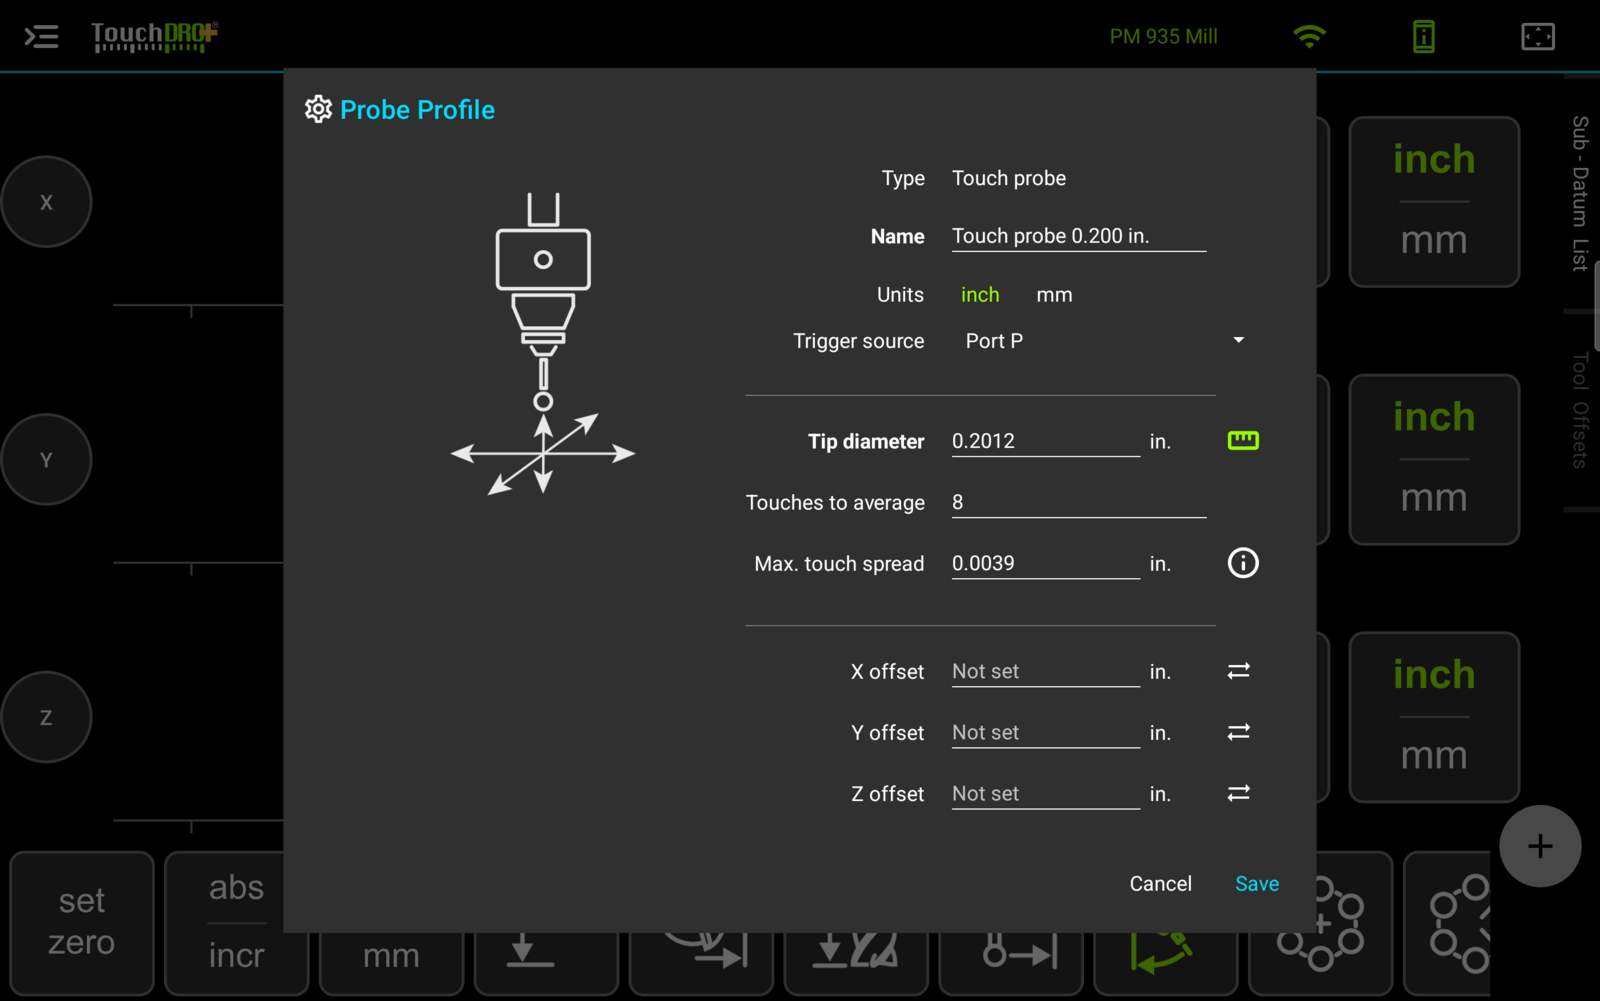
The Calibration Record
To open the stored run, press the information button beside "Max. touch spread" in the profile.
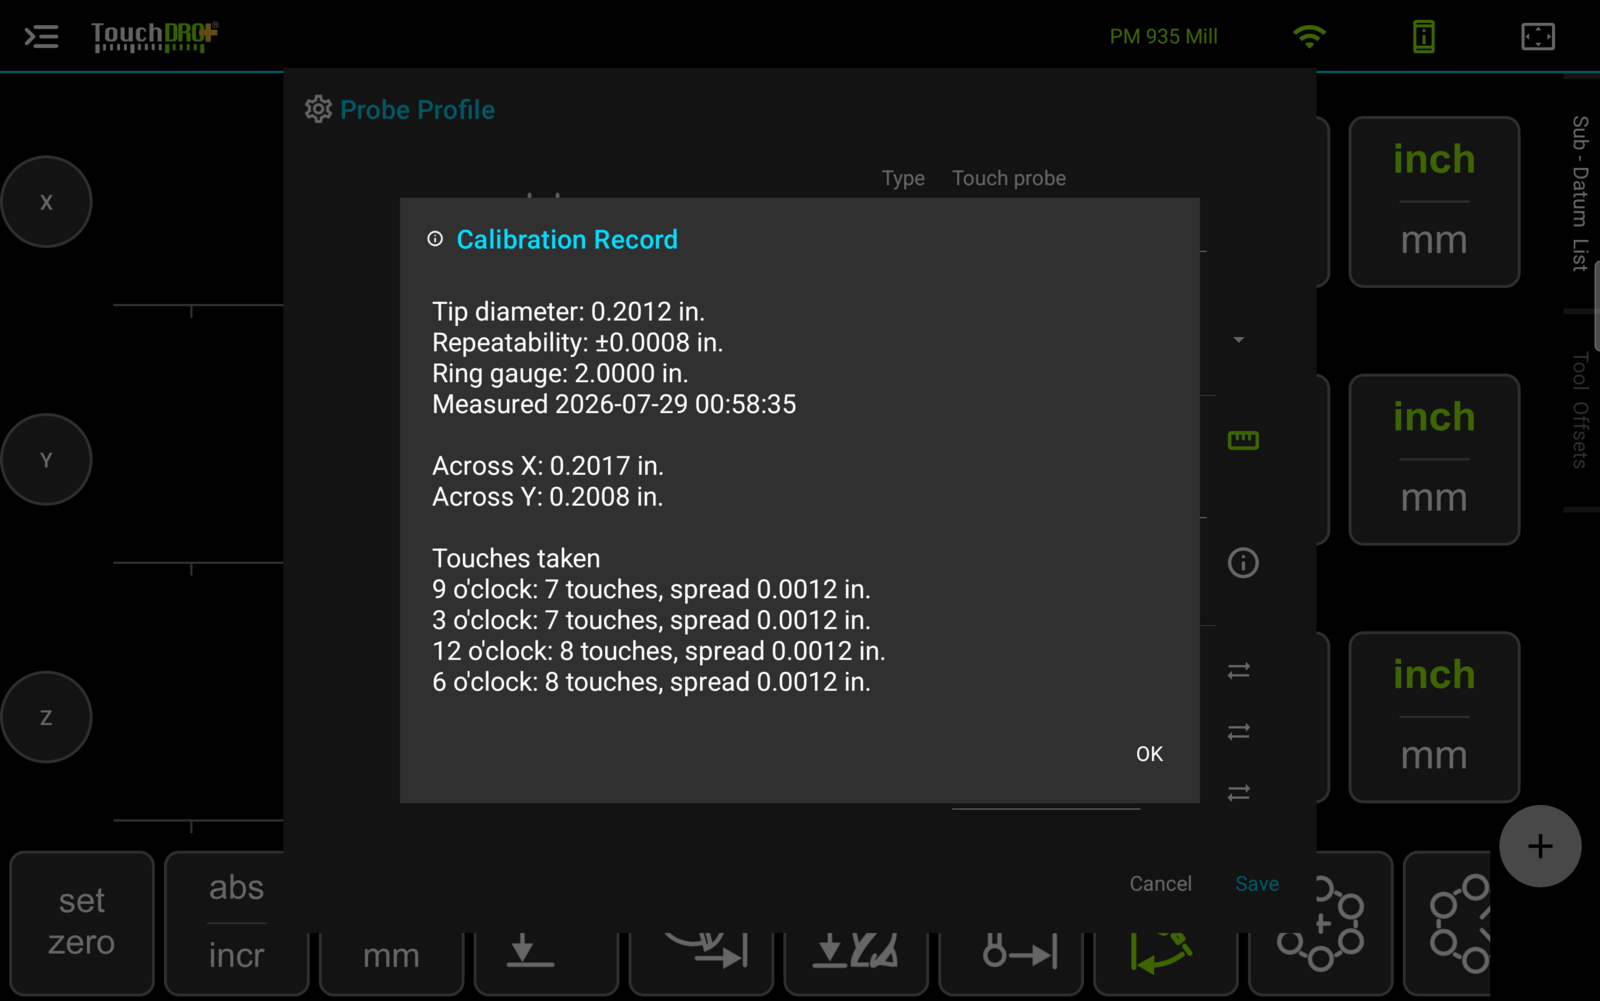
In addition to the values from the result, the record shows two things that are not available anywhere else once the averaged diameter has been stored. "Across X" and "Across Y" are the effective diameters measured along each axis, and the per-position list gives the touch count and spread at each of the four clock positions.
Interpreting the Result
The result describes two separate things with different causes: whether the tip measures the same in every direction, and whether it measures the same thing twice.
Across X and Across Y
In a mechanical touch probe, the stylus rests on a three-point kinematic seat, commonly three rods resting in pairs of balls at 120 degrees to each other. How far the stylus deflects before the probe triggers depends on which way it is pushed, because the stylus doesn't pivot against those three points the same way in every direction. The four touches sample that variation, and the difference between "Across X" and "Across Y" shows how large it is.
A small difference is normal for this type of instrument and not worth chasing, but a large one is a reason to look at the probe itself, since a stylus that has worked loose or grit in the seat will exaggerate it.
Note that this is unrelated to runout, since nothing is spinning during calibration. A difference between X and Y is caused by the seat and has nothing to do with how the probe is clocked in the spindle.
Repeatability
The plus-or-minus value is how closely repeated touches at the same place agreed. Two things make it large.
The first is technique. Approaching the wall too fast registers the touch late, and on a manual machine the approach speed depends entirely on your hands, so uneven cranking shows up directly as scatter. A slow, even approach does more for this number than any setting.
The second is the probe. If the stylus doesn't return to exactly the same rest position after each touch, it triggers in a slightly different place every time. A worn or dirty kinematic seat does this, and so does a stylus that isn't properly tight.
What Counts as Good
No probe repeats perfectly. Even probes costing several thousand dollars show some scatter on a manual machine, because the repeatability they are sold on assumes a controlled approach speed that hand feed can't deliver. In other words, the number is a judgment call rather than a pass or a fail.
As a rule of thumb, the best probes repeat inside a single encoder count, and a good hobby or prosumer probe should manage about one count either way. Judge it against your own scales rather than against a number quoted elsewhere: one count is a micron on a 1-micron scale and five microns on a 5-micron scale, so the same probe looks very different depending on what it is measured with.